Inventory Forecasting: Methods and Best Practices for Manufacturers
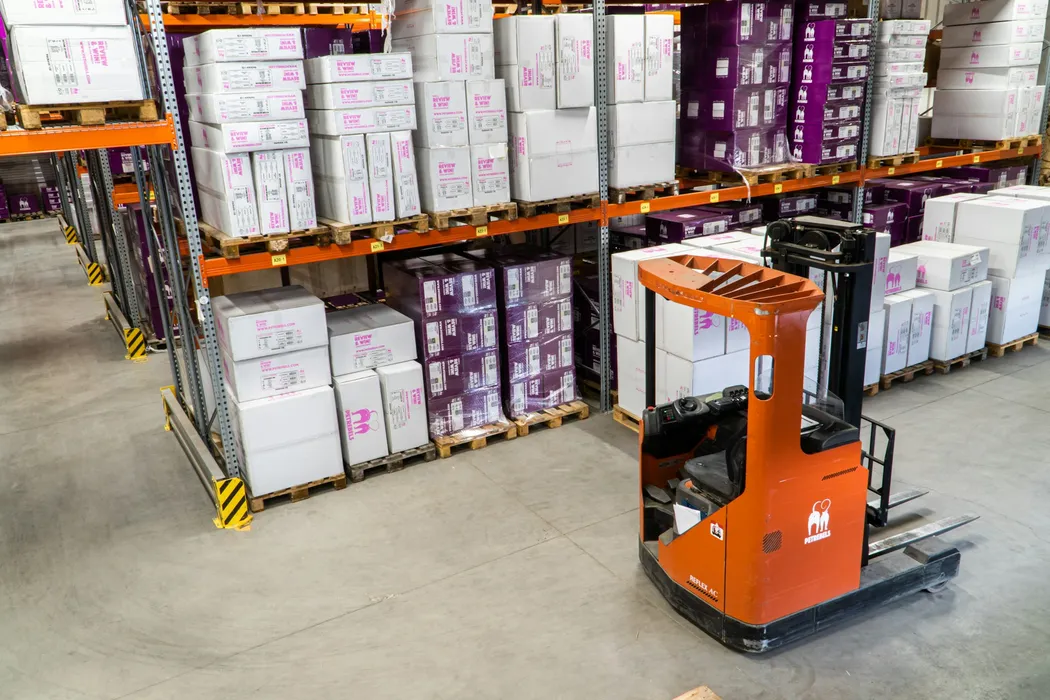
A single forecasting error can ripple through your entire production line. Overestimate demand and you tie up cash in excess inventory. Underestimate it and your production grinds to a halt while you wait for materials. For manufacturers, inventory forecasting is not just about predicting sales. It is about coordinating raw materials, subassemblies, production capacity, and finished goods across complex supply chains with lead times measured in weeks or months, not days.
What is Inventory Forecasting for Manufacturers?
Inventory forecasting is the practice of predicting future inventory needs using historical data, market trends, and production planning. For manufacturers, this process operates on two critical levels simultaneously. First, you forecast demand for finished goods based on customer orders, sales history, and market conditions. Second, you derive raw material requirements by working backward through your bill of materials.
This cascading calculation is the fundamental difference between manufacturing and retail inventory forecasting. A retailer predicts how many units to stock. A manufacturer must predict finished goods demand, then calculate exactly how many components, subassemblies, and raw materials are needed to produce those goods. When your bill of materials includes 50 components, a single finished goods forecast generates 50 dependent raw material forecasts.
The stakes are high. According to the National Association of Manufacturers, carrying costs for inventory typically range from 25 to 30 percent of inventory value annually. These costs include warehousing, insurance, obsolescence, and the opportunity cost of capital tied up in stock. Poor forecasting amplifies these costs while also risking production delays when materials run short.
Manufacturing inventory forecasting differs from simple replenishment. Replenishment is about reordering stock when it runs low. Forecasting is about predicting what you will need, when you will need it, and in what quantities, then planning production schedules and procurement accordingly. It requires balancing customer demand against production capacity, supplier lead times, and cash flow constraints.
5 Inventory Forecasting Methods for Manufacturing
Manufacturers can choose from several forecasting methods, each suited to different situations. The most effective approach often combines multiple methods to account for both historical patterns and real-world variables.
Quantitative Forecasting
Quantitative forecasting relies on historical sales and production data to predict future demand. This method works best for established products with predictable demand patterns. You analyze past sales volumes, identify trends, and project those patterns forward. For manufacturers, quantitative forecasting must account for production cycles, not just sales. If your production lead time is four weeks, your forecast needs to look ahead far enough to ensure materials arrive before production begins. The more historical data you have, the more accurate your quantitative forecast becomes.
Qualitative Forecasting
When historical data is limited or unreliable, qualitative forecasting fills the gap. This method uses market research, customer surveys, expert opinions, and sales team insights to estimate demand. Qualitative forecasting is essential for new product launches and custom manufacturing operations where each project is unique. For example, a furniture manufacturer launching a new product line would gather input from designers, sales representatives, and early customer feedback to build initial demand estimates.
Trend Forecasting
Trend forecasting examines how demand changes over time, identifying growth or decline patterns. This method helps manufacturers spot whether demand is increasing, decreasing, or holding steady. The key consideration for manufacturers is production capacity. You can forecast all the demand you want, but if your factory can produce only 1,000 units per month, forecasting demand for 1,500 units without a capacity expansion plan is meaningless. Trend forecasting can be top-down, starting with total market demand and working toward your share, or bottom-up, aggregating forecasts from individual product lines.
Seasonal Forecasting
Many manufactured products experience seasonal demand cycles. Furniture sales spike during back-to-school season and before holidays. Heating equipment sells in fall and winter, air conditioners in spring and summer. Seasonal forecasting uses historical patterns to predict these cyclical fluctuations. Manufacturers must plan production schedules to build inventory ahead of peak seasons without tying up excessive cash during slow periods. This often means ramping up production months before demand arrives.
Causal and Multi-Variable Forecasting
The most sophisticated approach, causal forecasting, incorporates external variables that influence demand. These might include raw material price fluctuations, supplier lead time changes, economic indicators, competitor actions, or regulatory changes. For manufacturers with complex, volatile supply chains, this method provides the most accurate forecasts. It requires more data and analytical capability but accounts for the real-world factors that can make or break a forecast.
Unlike retailers who forecast a single inventory level, manufacturers must forecast across multiple stages simultaneously. Your finished goods forecast cascades through your bill of materials, generating derived demand for subassemblies, components, and raw materials. This MRP cascade effect means a single error in finished goods forecasting multiplies through every level of your production process.
Try Controlata
- Manufacturing inventory management
- Cost calculation
- Production planning
- And much more
Key Formulas and Metrics Manufacturers Need
Several formulas help translate forecasts into actionable inventory decisions. These calculations determine when to reorder materials, how much to order, and how much safety stock to maintain.
Economic Order Quantity
The economic order quantity formula calculates the optimal order size that minimizes total inventory costs. The formula is EOQ = √(2DS/H), where D is annual demand in units, S is the cost per purchase order, and H is the holding cost per unit per year. For manufacturers, this applies primarily to bulk raw material purchasing. If you use 10,000 units of a component annually, each order costs $50 to process, and holding costs are $2 per unit per year, your EOQ is √(2 × 10,000 × 50 / 2) = 707 units per order.
Reorder Point
The reorder point determines when to place a new order. The formula is ROP = (daily usage × lead time in days) + safety stock. For manufacturers, lead time includes both supplier delivery time and your internal production lead time. If you use 50 units per day, your combined lead time is 10 days, and you maintain 100 units of safety stock, your reorder point is (50 × 10) + 100 = 600 units. When inventory drops to 600, you trigger a new purchase order.
Safety Stock
Safety stock is buffer inventory held to protect against demand variability and supply disruptions. The formula is: (maximum daily sales × maximum lead time) minus (average daily usage × average lead time). Manufacturers typically need higher safety stock than retailers because production risk compounds supply risk. Equipment breakdowns, quality issues, and process variations can consume additional materials beyond the forecast.
Sales Velocity versus Production Velocity
Sales velocity measures how quickly finished goods move through the sales pipeline. Production velocity measures how fast you can manufacture those goods. The gap between them reveals your constraint. If your sales velocity is 100 units per day but your production velocity is only 75 units per day, you have a capacity problem. No amount of forecasting will fix that gap without production improvements or additional capacity.
According to APICS research, manufacturers with optimized production planning systems reduce lead times by an average of 20 percent and improve on-time delivery rates to above 95 percent. These improvements stem from better alignment between demand forecasts and production capacity.
6 Challenges Unique to Manufacturing Inventory Forecasting
Manufacturing inventory forecasting faces obstacles that retailers never encounter. Understanding these challenges is the first step toward building more accurate forecasts.
Bill of Materials Complexity
A single finished product can require dozens or hundreds of components, each with its own lead time, supplier, and cost structure. When your bill of materials includes subassemblies that themselves require multiple components, forecasting becomes exponentially more complex. One error at the finished goods level cascades through every level of your BOM, potentially creating shortages or overstock across multiple materials simultaneously.
Production Capacity Constraints
Unlike retailers who can simply order more inventory, manufacturers are limited by production capacity. Equipment, labor, and floor space impose hard limits on how much you can produce in a given period. Your forecast must align with production scheduling. Forecasting demand beyond your capacity creates unfulfilled orders and customer dissatisfaction. Understanding your capacity constraints is as important as understanding demand.
Make versus Buy Decisions
Inventory forecasts directly influence whether to manufacture components in-house or purchase them from suppliers. Higher forecasted volumes might justify bringing production in-house. Lower volumes might favor outsourcing. These decisions affect capital investment, labor requirements, and inventory strategies, making forecasting a strategic decision beyond simple numbers.
Longer and More Variable Lead Times
Manufacturers often source raw materials from overseas suppliers with lead times of eight to twelve weeks or more. Custom components can take even longer. These extended lead times increase forecast uncertainty and require larger safety stock buffers. Lead time variability compounds the problem. When a supplier promises six weeks but delivers anywhere from five to nine weeks, forecasting becomes much harder.
Quality and Waste Factors
Production processes generate scrap and defects. If your historical scrap rate is five percent, you need to order 105 units of raw material to produce 100 finished units. Forecasts must incorporate these waste factors, which vary by product, process, and operator skill level. Ignoring scrap rates leads to material shortages mid-production.
Work-in-Progress Inventory
Partially completed goods tie up cash and warehouse space while providing no revenue. Managing WIP requires forecasting not just what to start producing, but also how production flows through your facility. Bottlenecks in one production stage create inventory pileups that throw off your entire forecast.
Research from the National Association of Manufacturers indicates that poor inventory management costs manufacturers two to three times more than retailers due to production downtime and changeover costs. When a production line stops because a forecasted part did not arrive, the costs include idle labor, unused equipment capacity, and missed delivery commitments.
Best Practices for Manufacturers
Effective inventory forecasting requires both the right tools and the right processes. These best practices help manufacturers build more accurate forecasts while adapting to changing conditions, and our MRP implementation guide for small manufacturers covers what the tooling side looks like in practice.
Use an MRP system designed for manufacturing. Manual spreadsheets collapse under the weight of complex bills of materials and multi-level inventory tracking. Modern systems like Controlata automate material requirements planning, track real-time inventory across multiple locations, and calculate production costs based on actual usage. They turn forecasting from a monthly spreadsheet exercise into an ongoing process integrated with production scheduling and procurement.
Collaborate across departments. Sales teams understand customer demand patterns. Production managers know capacity constraints. Procurement knows supplier reliability. Finance sets budget limits. Accurate forecasts require input from all these perspectives. Regular cross-functional meetings ensure everyone works from the same demand assumptions.
Factor in production capacity when forecasting demand. Do not forecast demand you cannot fulfill. If your capacity is 10,000 units per month, forecasting 15,000 units without a plan to expand capacity creates problems. Align your forecast with realistic production schedules and identify capacity bottlenecks before they become crises.
Monitor supplier performance closely. Late deliveries destroy even the best forecasts. Track supplier lead time variance and build relationships with backup suppliers for critical materials. When a key supplier is consistently late, increase safety stock or find alternatives.
Build in scrap rates and quality data. Historical scrap percentages should be part of your forecast model. If you typically lose three percent of a material to production waste, forecast accordingly. Ignoring waste leads to shortages.
Review and adjust forecasts monthly. Manufacturing conditions change constantly. New orders come in, suppliers change lead times, and production issues emerge. Treat forecasting as an ongoing process, not a set-it-and-forget-it annual exercise.
Segment products by lifecycle stage. New products need qualitative forecasting based on market research. Mature products with years of sales history can rely on quantitative methods. Use the right method for each product.
Maintain safety stock strategically. Holding safety stock on every item ties up too much cash. Use ABC analysis to identify which materials justify safety stock. Focus buffers on high-value items with long lead times or unreliable supply.
Conclusion
Inventory forecasting for manufacturers is fundamentally more complex than retail forecasting. The challenge is not just predicting customer demand but translating that demand through multi-level bills of materials while accounting for production capacity, supplier lead times, and waste factors. The payoff for getting it right includes reduced stockouts, lower carrying costs, improved cash flow, and smoother production operations. Start by evaluating your current forecasting process against the methods and best practices outlined here. Consider upgrading to a manufacturing-focused system that handles the complexity automatically. The best forecast is not the one with the most sophisticated algorithm. It is the one that balances historical data with real-world production constraints and gets updated as conditions change.